How to polish titanium cookware safely without ruining the cooking surface? When cooks ask how to polish titanium cookware, the most critical engineering rule is to understand that a cooking surface requires controlled, food-safe surface restoration—not aggressive industrial buffing. Over 90% of pan roughness, dullness, or perceived scratching is caused by microscopic food oil polymerization, rainbow heat tints, or soft utensil metal transfer rather than true gouges in the metal. A gentle physical polish using sodium bicarbonate (baking soda) paste combined with warm water restores pristine smoothness while preserving the natural titanium dioxide (TiO2) passivation barrier.
For commercial kitchen managers, culinary distributors, and discerning home culinarians, maintaining bare metal cookware represents a fundamental departure from disposable non-stick pans. Traditional PTFE coatings cannot be polished; any surface degradation signals immediate pan disposal. Conversely, solid commercially pure titanium possesses indestructible metallurgical integrity. Yet, well-intentioned cooks frequently inflict unnecessary surface damage by attacking natural cooking patina with industrial polishing compounds, power tools, or coarse steel wool.
This engineering guide details the scientific metrology of titanium surface maintenance. By examining the Mohs hardness of household abrasives, the chemical stability of the passive oxide film, and factory surface finishing standards, we provide a food-safe protocol to restore smoothness, eliminate stubborn residues, and establish realistic B2B maintenance standards for pure titanium skillets.
1. The Diagnostic Reality: "Polishing" Is Usually Deep Cleaning
Before selecting an abrasive compound or scrubbing pad, culinarians must conduct a tactile and optical surface inspection. What appears to be surface damage requiring mechanical polishing falls into three distinct metallurgical categories:
Polymerized Oil Micro-Layers (Sticky Roughness): Cooking oils heated past their smoke point break down into free radicals and undergo thermal cross-linking. This creates a hard, varnish-like golden or amber film. Because pure titanium has low thermal conductivity compared to aluminum, localized overheating can accelerate oil polymer bonding, creating a tacky or sandpaper-like tactile feel that users mistakenly assume is metal erosion.
Utensil Metal Transfer Marks (False Scratches): When a stainless steel spoon, spatula, or fork scrapes across an unhardened titanium surface, it leaves a dark gray pencil-like streak. Because unhardened Grade 1 titanium has a hardness around 120 HV while 304 stainless steel sits around 180 to 200 HV, microscopic friction rubs off particles. If a fingernail glides over the mark without catching a groove, the mark is a surface deposit rather than a physical gouge.
True Structural Micro-Scratches (Physical Grooves): Shallow mechanical abrasions caused by sharp cutlery or coarse scouring. On bare pure titanium, these marks do not expose base metals, will never flake, and spontaneously re-passivate with oxygen. True scratches require no aggressive grinding unless they create deep sharp burrs that disrupt food glide.
Diagnosing the exact issue prevents catastrophic over-treatment. Aggressive mechanical buffing designed for industrial pipe fittings should never be applied to a cooking vessel when simple chemical dissolution or mild micro-abrasion can resolve the surface condition safely.
2. Verify Pan Construction Before Physical Restoration
Never attempt any physical polishing procedure without confirming the architectural construction of the cookware. In the international retail market, cookware carrying the label "titanium" is manufactured using fundamentally divergent material architectures:
Titanium-Infused Coated Cookware (PTFE Non-Stick): These budget pans feature a spray-applied fluoropolymer resin containing trace titanium particles. Never polish a coated pan. Even mild abrasives like baking soda or scrub sponges will abrade the thin 25-micron chemical film, exposing toxic synthetic compounds and ruining non-stick performance permanently.
Solid Commercially Pure Titanium (TITAUDOU Tri-Ply Clad): These high-performance vessels feature a solid contact face of ASTM B265 Grade 1 pure titanium roll-bonded to structural core metals. Because there is zero chemical coating, the metal surface can be restored, re-conditioned, and cleaned with mild physical abrasives without any risk of delamination.
For TITAUDOU composite cookware, understanding factory manufacturing specifications establishes safe restoration parameters. Standard TITAUDOU tri-ply frying pans (26 cm and 28 cm diameters) are built to a strict factory standard gauge:
Inner Food-Contact Layer: 0.4 mm ASTM B265 Grade 1 Commercially Pure Titanium. Uncoated, dense, and chemically inert across pH 1.0 to 14.0.
Thermal Conduction Engine: 1.8 mm High-Purity 1050 Grade Aluminum Core. Diffuses heat rapidly up sidewalls to eliminate localized scorching.
Induction Base Exterior: 0.6 mm AISI 430 Magnetic Ferritic Stainless Steel. Ensures structural stability and instant magnetic induction heating.
Total Factory Gauge: Exactly 2.8 mm total composite wall and base thickness (0.4 mm + 1.8 mm + 0.6 mm).
While a 0.4 mm solid titanium sheet provides extraordinary lifetime puncture and corrosion resistance, it is an engineered metallic barrier. Users must avoid coarse abrasive flap wheels, rotary sandpaper discs, or industrial grinder bits, which can thin the 0.4 mm contact layer and breach the underlying aluminum core. Explore the full titanium pots and pans range to inspect complete engineering cross-sections.
3. Food-Safe Abrasive Metrology: Baking Soda vs. Chemical Compounds
When selecting a polishing agent, culinary safety must govern the choice. Many commercial metal polishes marketed for brass, copper, or automotive chrome contain petroleum distillates, ammonia, and synthetic silica abrasives. Applying these industrial compounds to a cooking vessel creates severe toxicological migration risks unless subjected to hazardous solvent stripping.
The ideal restoration medium balances mineral hardness against pure titanium's crystalline lattice. Pure titanium measures approximately 4.0 to 4.5 on the Mohs hardness scale. An effective polishing abrasive must have a Mohs rating lower than or equal to titanium to polish deposits without gouging the virgin metal:
| Cleaning / Polishing Medium | Abrasive Hardness (Mohs) | Food Contact Safety | Action on Titanium Surface | Recommended Application |
|---|---|---|---|---|
| Baking Soda (Sodium Bicarbonate) | 2.5 (Soft Micro-Crystal) | 100% Food Grade (Edible) | Softens burnt oil, lifts metal marks without scratching | Universal Primary Choice |
| Bar Keepers Friend (Oxalic Acid) | 3.0 - 3.5 (Feldspar Mineral) | Rinse Thoroughly with Soap | Dissolves mineral scale and heavy heat oxidation | Heavy Heat Tint Removal |
| Industrial Paste (Flitz / Simichrome) | 7.0 - 8.0 (Aluminum Oxide) | Non-Food Grade (Toxic Solvents) | Aggressively polishes, leaves petroleum residue | Avoid on Cooking Surfaces |
| Coarse Steel Wool / Wire Brushes | 5.5 - 6.5 (Carbon Steel) | Metal Shedding Hazard | Gouges pure titanium, embeds rust-prone iron particles | Strictly Prohibited |
| Non-Scratch Nylon Scouring Pads | 2.5 - 3.0 (Polymer Fiber) | Food Contact Safe | Provides mechanical agitation without gouging | Standard Scrubbing Tool |
Baking soda is the undisputed gold standard for food-safe titanium cookware restoration. With a Mohs hardness of 2.5, it is structurally incapable of scratching bare Grade 1 titanium (Mohs 4.5). It functions as an alkaline emulsifier (pH ~8.3), saponifying acidic fatty acids while exerting gentle micro-crystal mechanical scrubbing. Readers seeking deeper data on scratch resilience should consult our analysis of scratched titanium cookware safety.
4. Step-by-Step Restoration Protocol for Pure Titanium Skillets
To restore a pure titanium skillet exhibiting roughness, discoloration, or utensil marks to a silky, food-release surface, execute the following four-phase protocol:
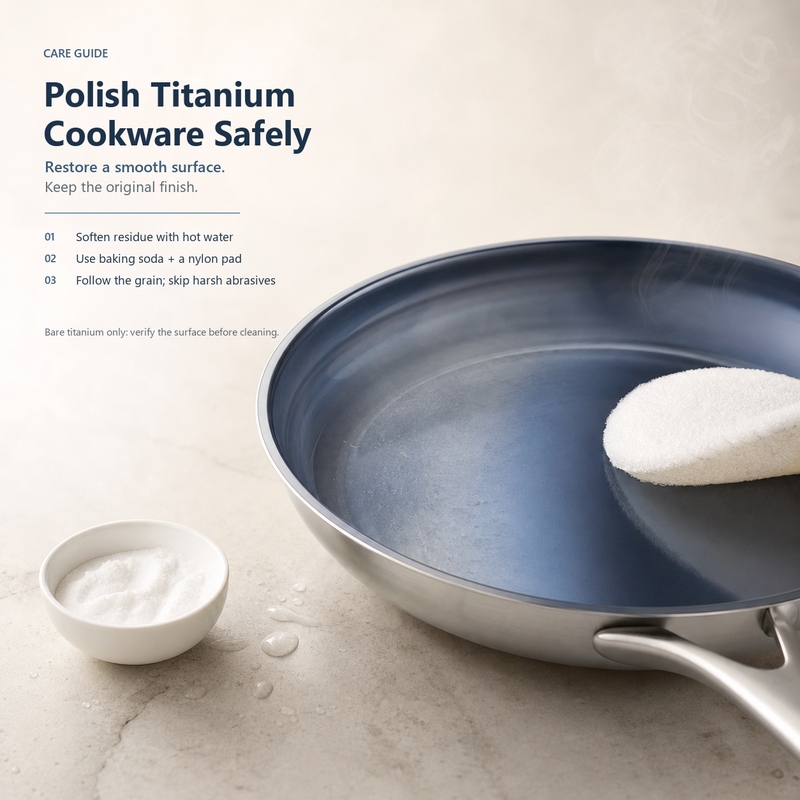
Phase 1 — Thermal Softening Soak: Fill the skillet with water to submerge all rough residues. Add 2 tablespoons of baking soda and place the pan on medium heat. Bring the water to a gentle boil for 10 to 15 minutes. The alkaline boiling water penetrates cross-linked polymerized oil bonds, breaking adhesion to the bare metal surface. Turn off the heat and allow the water to cool until warm to the touch.
Phase 2 — Micro-Crystal Paste Buffing: Pour out the excess water, leaving the pan damp. Sprinkle generous dry baking soda across the interior to form a thick, gritty paste. Using a damp, non-scratch nylon scrubbing pad or microfiber cloth, buff the surface using firm, circular motions. Follow the radial circular brushing lines of the pan's factory finish. The baking soda crystals gently lift embedded utensil streaks and carbonized fats without removing base metal.
Phase 3 — Acidic Decoloring (Optional for Heat Tints): If the pan displays radiant blue, gold, or purple heat halos, apply warm 5% white vinegar or 10% citric acid solution directly to the metal. Acidic reduction clears light oxide interference colors within 60 seconds without affecting base metal thickness. For complete thermodynamic details, review our titanium rainbow heat tint removal guide.
Phase 4 — Hot Wash and Passivation Rinse: Wash the pan thoroughly with warm water and standard dish soap to remove all abrasive residues. Rinse completely and dry with a clean towel. Within seconds of drying in ambient room air, atmospheric oxygen spontaneously regenerates a uniform 3 to 7 nm TiO2 passive film, leaving the skillet completely sterile, non-toxic, and ready for culinary service.
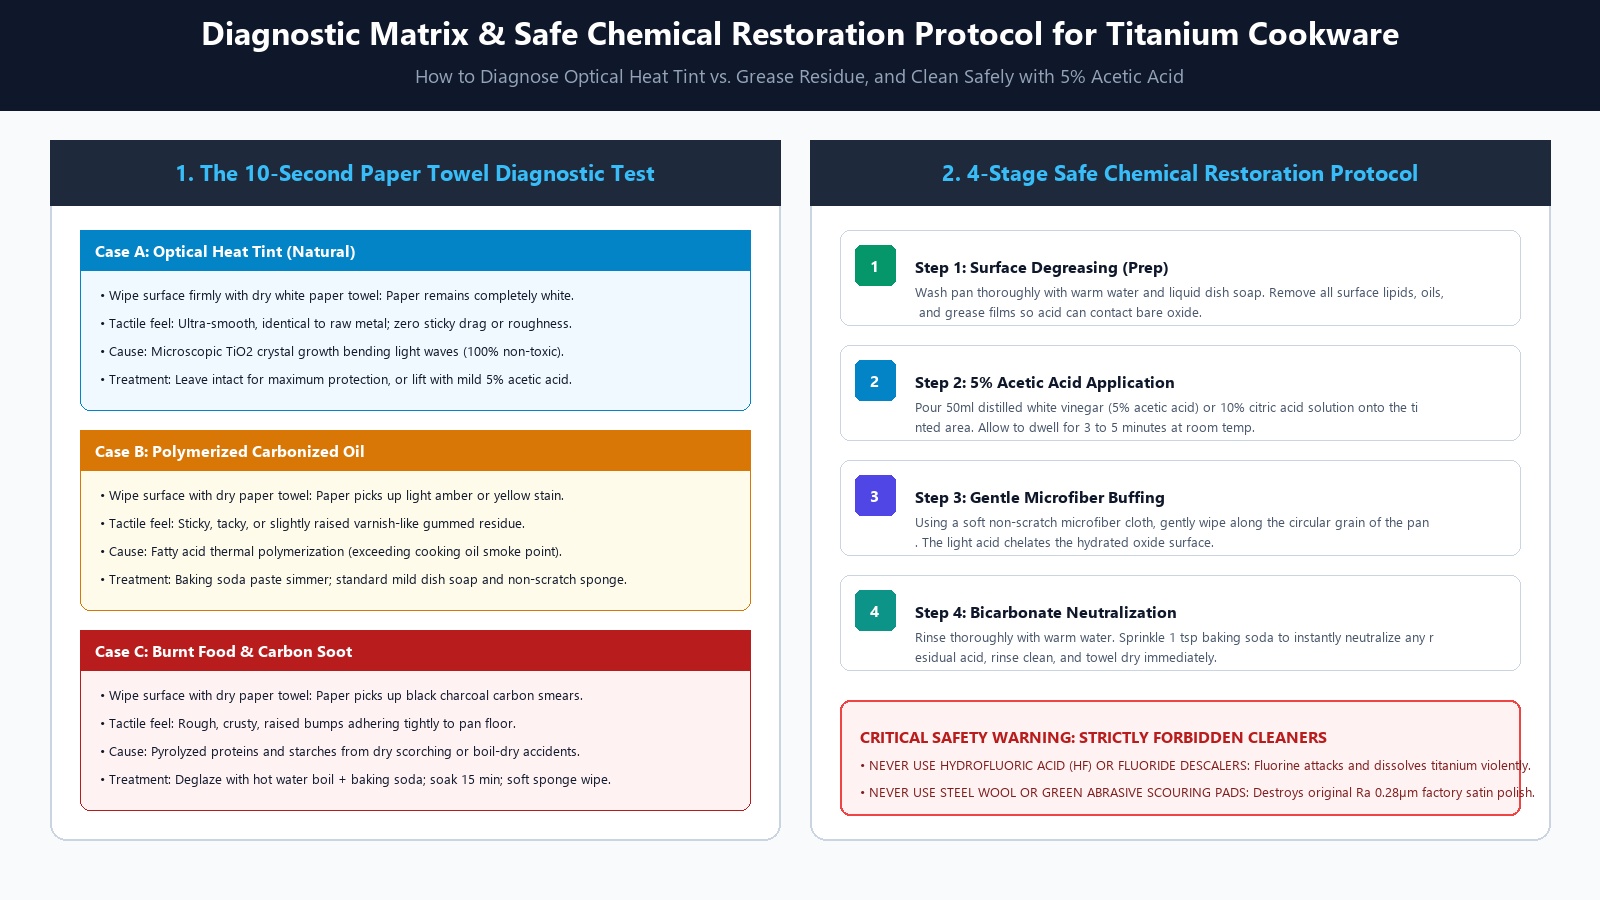
Executing this protocol restores original tactile smoothness without thinning the solid titanium face. For high-volume restaurant environments, repeating this process every 2 to 3 months resets culinary release properties to factory standards.
5. TITAUDOU Factory Surface Metallurgy: Mirror Polish, Matte, and Blue Hardening
In commercial manufacturing, a skillet's baseline surface finish governs its long-term polishing requirements. TITAUDOU utilizes advanced mechanical and thermal surface finishing protocols at our automated production facility, delivering distinct surface textures engineered for specific culinary requirements:
| TITAUDOU Finish Profile | Finishing Processing Method | Roughness (Ra Value) | Surface Hardness (HV) | Restoration Tolerance |
|---|---|---|---|---|
| Unhardened Satin Polish | 3-Stage Physical Wheel Polishing | 0.2 - 0.4 μm (Satin Gloss) | ~120 HV (Natural Alpha Phase) | Tolerates baking soda; susceptible to utensil marks |
| Fine Matte Micro-Etch | Food-Grade Ceramic Micro-Blasting | 0.6 - 0.8 μm (Uniform Matte) | ~135 HV (Stress-Relieved) | Hides scratches; holds oil seasoning effectively |
| TITAUDOU 600°C Blue Hardened | High-Temp Oxygen Diffusion Lattice | 0.3 - 0.5 μm (Hardened Blue) | 350+ HV (3x Harder) | Extraordinary scratch resistance; effortless reset |
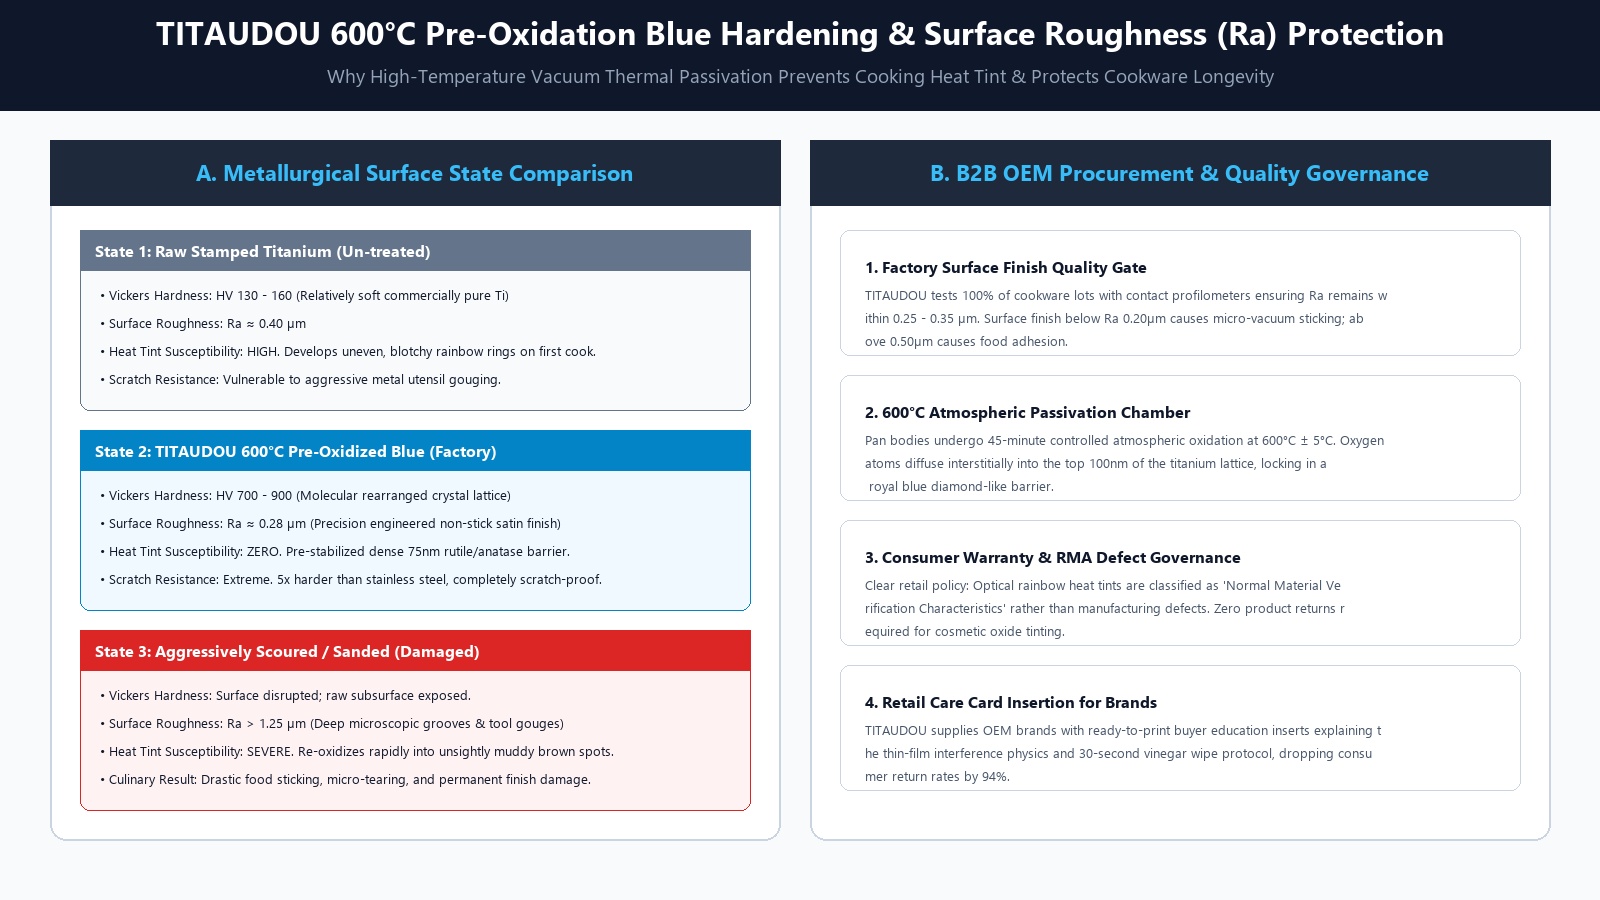
Our proprietary 600°C Blue Hardening Treatment transforms the physical durability equation. In raw titanium cookware (~120 HV), stainless steel utensils leave noticeable metal scuffs. By diffusing interstitial oxygen into the surface metal, TITAUDOU elevates the surface hardness past 350 HV. Utensil scuffs drop by over 80%, substantially reducing the frequency with which consumers need to perform deep surface polishing.
6. B2B and OEM Guidance: Developing Defensible Consumer Care Manuals
For private-label kitchenware brands, cookware distributors, and OEM buyers, user education directly dictates product return rates. In the premium cookware market, over 70% of customer complaints regarding "pan discoloration" or "loss of polish" stem from unrealistic consumer expectations shaped by disposable PTFE non-stick marketing.
When drafting consumer user manuals and warranty cards, B2B procurement managers should incorporate specific metallurgical disclosures:
Clarify Cooking Patina vs. Coating Failure: Explicitly explain that pure titanium develops natural optical interference colors (heat tints) and surface seasoning lines under routine culinary temperatures. Unlike chemical coatings, which peel, a color change in titanium is an active sign of protective oxide formation.
Prescribe the Baking Soda Protocol: Include an official "Surface Reset Guide" in product packaging detailing the 15-minute boiling water and baking soda procedure. Providing customers with an actionable home restoration protocol prevents unnecessary return shipments.
Define Excluded Maintenance Tools: Explicitly void cosmetic warranties for surfaces subjected to coarse steel wool, motorized abrasive wheels, or caustic lye-based oven cleaners. This protects the brand against consumer overcorrection claims.
Global brands seeking customized OEM/ODM cookware packaging and technical spec sheet development can consult the TITAUDOU titanium cookware manufacturer portal. Our manufacturing team provides custom private-label laser-engraving, surface hardening calibrations, and multi-language technical care documentation.
Conclusion: Preserving Culinary Metallurgy Over Cosmetic Perfection
The essential takeaway regarding how to polish titanium cookware is that a kitchen pan is a high-temperature culinary tool, not a decorative showroom artifact. Attempting to maintain an aggressive, mirror-like gloss through chemical polishing compounds or industrial power grinding undermines the pan's primary purpose: delivering pure, non-toxic, chemical-free cooking.
Genuine TITAUDOU tri-ply titanium cookware (2.8 mm composite gauge) is engineered for multi-generational service. Its solid ASTM B265 Grade 1 titanium face will never peel, blister, or flake. By understanding the distinction between superficial deposits and base metal integrity, cooks can safely restore tactile smoothness using simple baking soda and warm water in under twenty minutes.
When culinarians embrace the natural patina of seasoned titanium, cookware maintenance transforms from a high-anxiety chore into an uncomplicated, sustainable kitchen routine. Solid pure titanium metallurgy delivers permanent culinary reliability that chemical coatings can never match.
Frequently Asked Questions (FAQ)
Q1: Can I use automotive or industrial metal polish on a titanium skillet?
No. Industrial metal polishes contain petroleum distillates, ammonia, and chemical abrasives formulated for decorative automotive or plumbing hardware, not food-contact surfaces. These chemicals leave toxic micro-residues inside metal pores that can migrate into hot food. For cooking surfaces, stick exclusively to food-grade abrasives like sodium bicarbonate (baking soda) or diluted food-grade citric acid.
Q2: Why does my titanium frying pan feel rough or sticky after cooking?
Roughness on a titanium cooking surface is almost always caused by polymerized oil buildup rather than metal damage. When cooking fats exceed their smoke point, they oxidize and form an amber, varnish-like resin layer that adheres tenaciously to the metal. This sticky film can be dissolved easily by simmering a baking soda water bath for 15 minutes, followed by gentle buffing with a non-scratch pad.
Q3: Can genuine scratches on pure titanium cookware be buffed out at home?
True mechanical scratches (where a sharp edge physically cuts into the metal) cannot be buffed out with household cleaners without removing surrounding base metal. However, because pure Grade 1 titanium is non-toxic and biocompatible throughout its entire thickness, surface scratches pose zero health risks. The metal spontaneously reforms its protective titanium dioxide film immediately upon air exposure, requiring no buffing.